
SMC Servo CNC Moulding Press
The SMC servo CNC moulding press is designed for sheet moulding compound (SMC) compression moulding. The servo system provides accurate closed-loop control of pressure and speed, together with mould-temperature control to improve flow and filling and reduce short shots and bubbles. It is suitable for electrical and automotive structural parts.
Get a Quote →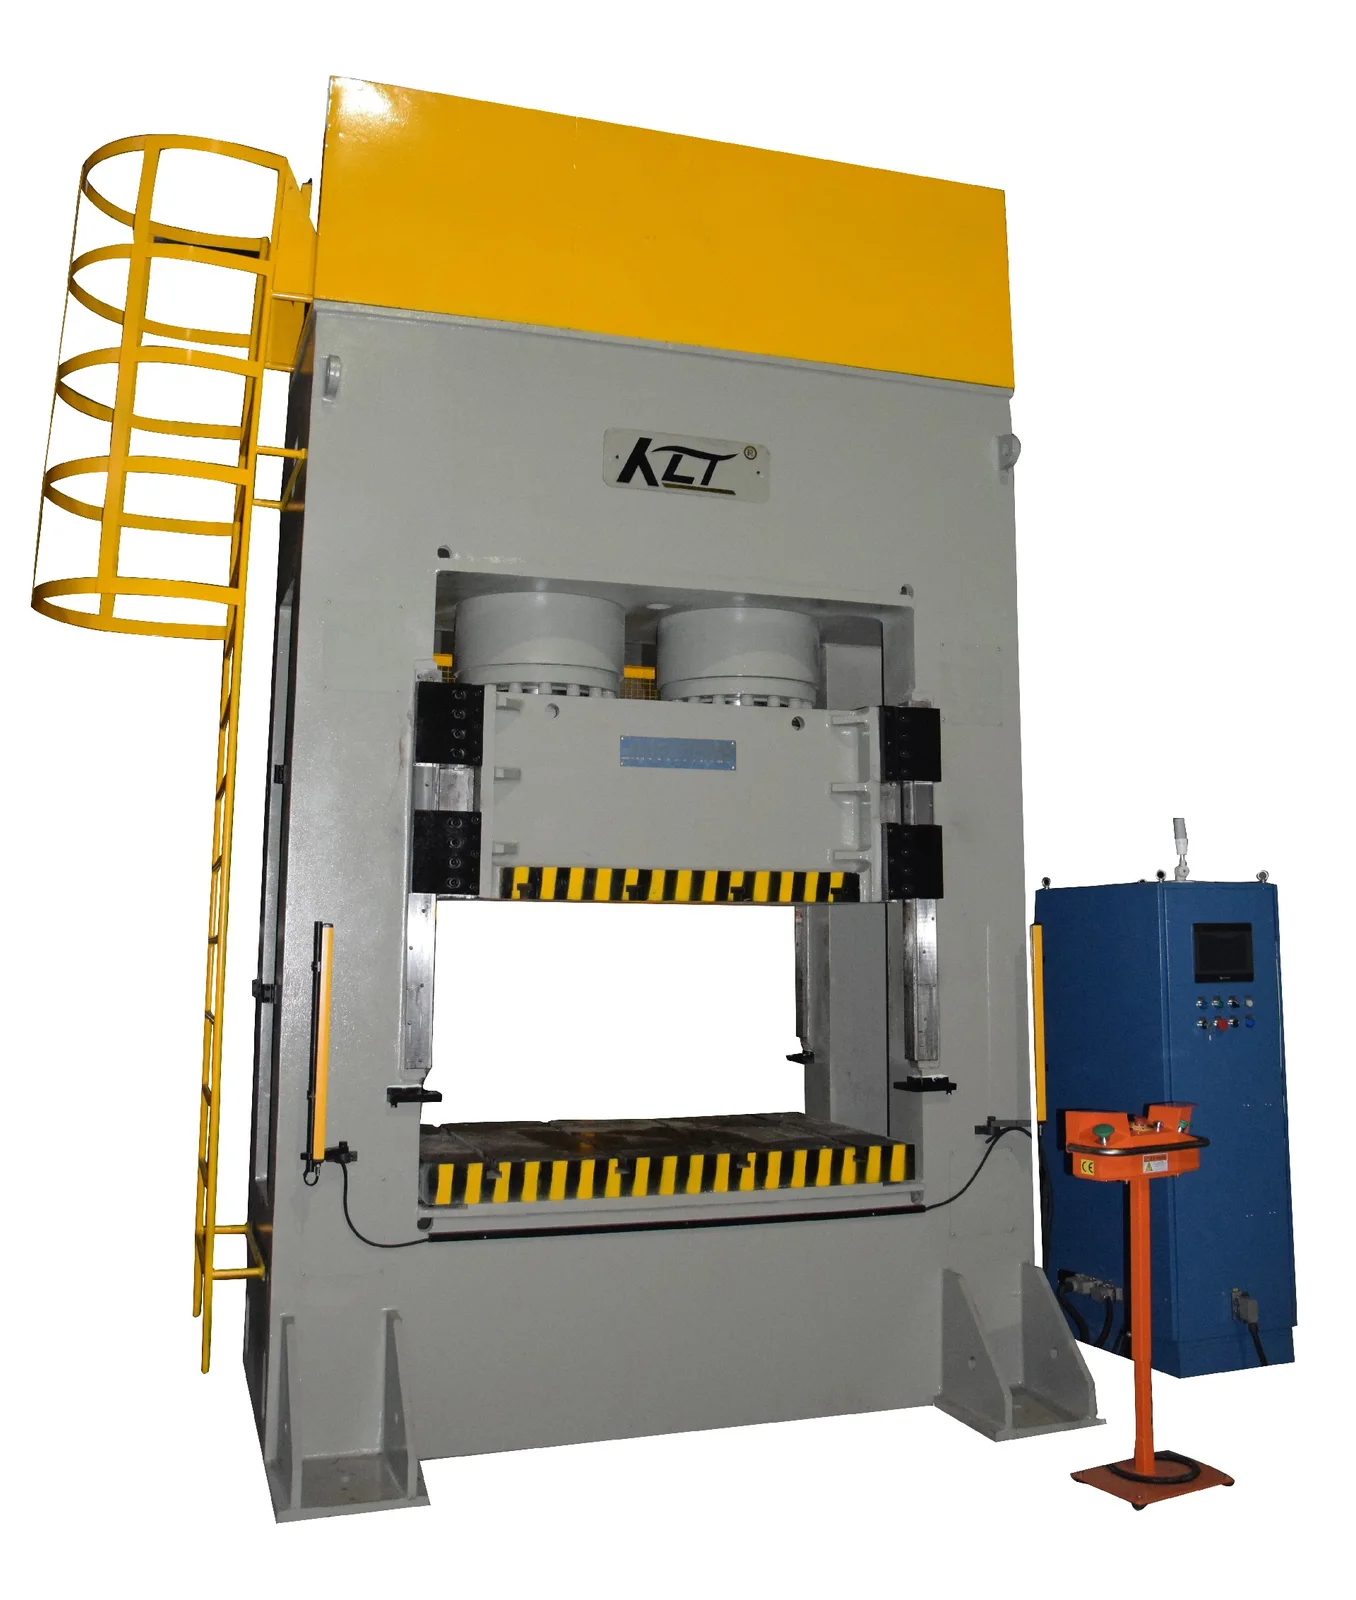
Product Introduction
The HPHS series SMC material hot-forming press adopts full CNC servo control. During SMC product forming, the press can set the pressure value, speed, position, holding time and mould-opening speed at will for each product.
Lay the SMC sheet material flat on the lower mould. After the upper and lower moulds are closed and sealed, apply a delayed pressure hold. Mould heating uses a mould-temperature controller to keep the temperature accurate. On a dedicated SMC forming hydraulic press, the prepreg is cured under high temperature and pressure for a set time, then the SMC part is removed from the mould and finished by trimming the flash. This moulding process offers high strength, high precision, light weight, low sensitivity to the environment and easy batch production, and is suitable for batch and standardised part production.
Equipment features:
1. Accurate control of pressure values
2. Accurate control of speed and position
3. Edit and save programs for product numbers at will
4. Accurate control of heating-platen temperature
5. High-efficiency deodorisation and purification system
Scope of Application
Applicable materials: SMC/BMC/DMC/GMT
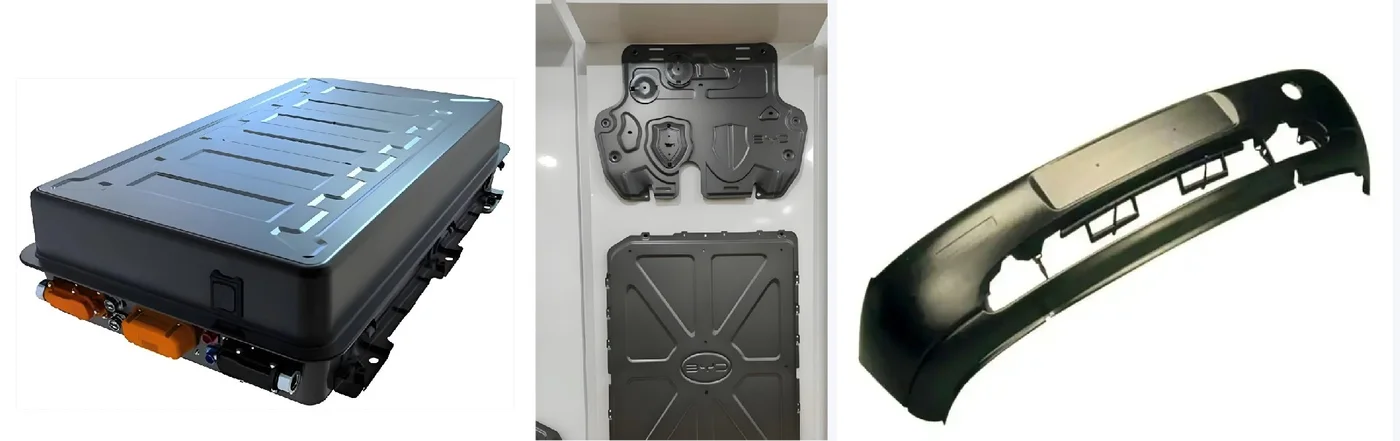
Applicable products: automotive bumpers, NEV battery cases, automotive guards, battery enclosures, energy-storage enclosures, etc.
| Item | Unit | 100T | 200T | 315T | 500T | 630T | 1000T | 1500T | 2000T |
|---|---|---|---|---|---|---|---|---|---|
| Nominal force | KN | 1000 | 2000 | 3150 | 5000 | 6300 | 10000 | 15000 | 20000 |
| Fluid pressure | Mpa | 25 | 25 | 25 | 25 | 25 | 25 | 25 | 25 |
| Slider stroke | mm | 600 | 800 | 800 | 1200 | 1200 | 1600 | 1600 | 2000 |
| Daylight (opening height) | mm | 900 | 1200 | 1200 | 1600 | 1600 | 2000 | 2000 | 2000 |
| Ejecting stroke | mm | 150 | 170 | 180 | 180 | 180 | 200 | 220 | 250 |
| Preload pressure | KN | 315 | 630 | 1000 | 1500 | 2000 | 3150 | 5000 | 6300 |
| Opening mould force | KN | 200 | 400 | 630 | 1000 | 1250 | 2000 | 3150 | 4000 |
| Demould force | KN | 100 | 200 | 500 | 500 | 500 | 500 | 500 | 500 |
| Down speed | mm/s | 200 | 200 | 200 | 200 | 200 | 300 | 300 | 300 |
| Working speed | mm/s | 1—6 | 1—6 | 1—6 | 1—6 | 1—6 | 0.5—5 | 0.5—5 | 0.5—5 |
| Return speed | mm/s | 100 | 100 | 100 | 150 | 150 | 200 | 200 | 200 |
| Preload speed | mm/s | 6—25 | 6—25 | 6—25 | 6—25 | 6—25 | 5—30 | 5—30 | 5—30 |
| Demould speed | mm/s | 5—30 | 5—30 | 5—30 | 5—30 | 5—30 | 5—30 | 5—30 | 5—30 |
| Table size, left–right | mm | 630 | 900 | 1200 | 1400 | 1600 | 3200 | 3200 | 3200 |
| Table size, front–back | mm | 630 | 900 | 1200 | 1400 | 1600 | 2200 | 2200 | 2500 |
| Main pump power | KW | 11 | 18.5 | 30 | 45 | 75 | 110 | 180 | 230 |
| Weight | T | 4.2 | 12 | 22.5 | 43.5 | 56 | 112 | 162 | 222 |
Equipment images and parameters are supplied product references. Final configuration and process performance are confirmed in the technical proposal.