
Carbon-Fiber Prepreg Multi-Daylight Hot Press
The carbon-fiber prepreg dedicated lamination hot press is used for laminating and curing unidirectional and fabric prepreg. Multi-stage temperature–pressure curves combined with uniform pressing control resin flow and resin content, improving laminate density and surface quality.
Get a Quote →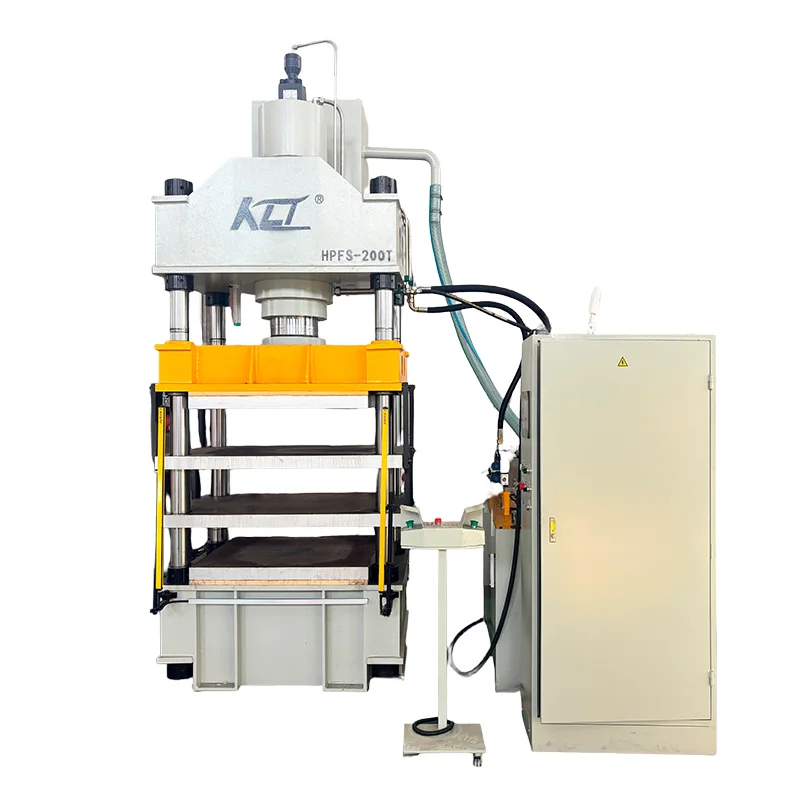
Product Overview
KLT's carbon-fiber prepreg dedicated lamination hot press is a high-precision hydraulic forming machine custom-developed for continuous/batch carbon-fiber prepreg lamination, resin-impregnation curing and composite-plate densification. Focused on the core pain points of prepreg production, it integrates three core systems — servo energy-saving hydraulics, staged temperature–pressure coordination and full-area vacuum de-bubbling — precisely solving industry problems of traditional equipment such as uneven pressure, bubble delamination, large resin-impregnation deviation and low yield.
The machine is designed for new-energy lightweight components, rail transit, aviation support and industrial-robot carbon-fiber prepreg mass production. Compatible with multiple matrix materials such as epoxy and phenolic resins, it supports multi-layer synchronous hot pressing and custom process-curve storage, and is the core forming equipment for standardised mass production in mid-to-high-end carbon-fiber composite enterprises.
Adaptation to Industry Pain Points (precisely solving prepreg production problems)
Pain point 1: large pressure fluctuation → uneven resin impregnation, dry-fiber defects. The whole machine is rigidly reinforced, with full-platen pressure uniformity of ±2% and uniform full-area infiltration, eliminating local resin shortage.
Pain point 2: inter-layer trapped air → high porosity, degraded mechanical properties. A front-end vacuum de-bubbling system controls porosity within ≤0.5%, improving inter-layer shear strength.
Pain point 3: unsynchronised temperature and pressure → poor batch consistency. PLC staged programmable temperature and pressure control accurately matches the prepreg curing curve.
Pain point 4: high energy use and cumbersome maintenance. Servo on-demand oil supply saves energy; a local modular structure makes maintenance convenient and low-cost.
Pain point 5: small platen and low load → limited capacity. A large-platen anti-eccentric-load design supports multi-layer synchronous forming, greatly increasing single-batch capacity.
Core Configuration and Product Advantages
1. Heavy-duty Precision Frame, Stably Outputting 200 T Rated Forming Pressure
An integral welded high-strength frame plus a precision four-column guide structure offers excellent anti-eccentric-load and anti-deformation capability, suitable for high-pressure forming of thick, multi-layer carbon-fiber billets. Rated pressure 200 T, forming pressure covering the 5–10 MPa prepreg standard-process range, with full-platen pressure uniformity within ±2%, ensuring consistent resin infiltration across the whole prepreg sheet.
2. Multi-Stage Temperature–Pressure Coordination Control System, Process Traceable and Replicable
Equipped with an industrial PLC touch-screen control system supporting fully programmable customisation of the whole process of multi-stage heating, holding, pressing, pressure holding, pressure relief and cooling. Hundreds of prepreg-specific process parameters can be stored and recalled with one click when switching products; it clearly distinguishes the three process stages of low-temperature resin flow, medium-pressure impregnation and high-temperature cross-linking cure, thoroughly solving the adaptation difficulty of different-viscosity resins and greatly improving batch-product consistency.
3. Integrated Vacuum-Assisted Forming System, Eliminating Bubble Delamination Defects
Full-area vacuum extraction before hot-press closing quickly discharges trapped air between carbon-fiber laminate tows and inter-layers; finished-prepreg porosity is controlled within 0.5%, effectively avoiding later-part delamination, cracking and fatigue failure, meeting aerospace and new-energy high-end supply-chain access standards.
4. Servo Energy-Saving Hydraulic Power, Reducing Cost and Increasing Efficiency for Mass Production
A servo variable-frequency hydraulic system dynamically matches flow and pressure to process needs, with no no-load energy waste. Compared with traditional fixed-displacement-pump hydraulic equipment, overall energy consumption is reduced by 18%; the hydraulic circuit uses a composite-industry dedicated modular design with low seal and valve-group wear, lowering average annual maintenance cost by over 35% versus imported equipment.
5. Local Full-Chain Service, Process Empowerment + Rapid After-Sales
Delivered locally from the Wuxi factory, with on-site installation and calibration, process-parameter commissioning and full-process operator training; a dedicated technical team handles composite-forming process optimisation, providing not only equipment but also prepreg mass-production forming solutions, responding to after-sales needs within 2 hours so as not to interrupt mass-production rhythm.
Standard Technical Parameters
| Parameter | Specification |
|---|---|
| Rated force | 200T |
| Table effective size | Custom sizes to suit prepreg width |
| Pressure uniformity | ≤±2% |
| Max. working temperature | 350 °C, independently controlled zones |
| Temperature control accuracy | ≤±1℃ |
| Vacuum level | ≤-0.095MPa |
| Forming porosity | ≤0.5% |
| Control method | PLC touch screen; programmable multi-stage process |
| Power system | Servo hydraulic system |
| Compatible resin systems | Epoxy, phenolic and high-temperature modified resins |
Application Process Flow
Billet lamination: cut carbon-fiber fabric, laminate multiple layers by fiber orientation and resin ratio and assemble.
Loading and clamping: precisely position on the work table, close the platen and seal the cavity.
Vacuum de-bubbling: full-area vacuum extraction discharges trapped air between layers and inside tows.
Staged hot pressing: complete heating → impregnation → high-pressure cure → constant-temperature holding along the preset curve.
Holding and cooling: closed-loop temperature-controlled cooling to avoid finished-part warping.
Discharge and inspection: inspect finished-part flatness, resin content and mechanical properties, then stock.
The whole process runs as an automated closed loop with no manual intervention in key processes, greatly reducing human error and suitable for scaled continuous mass production.
Mass-Production Results (user evidence)
Measured data from a Wuxi (carbon-fiber prepreg mass-production enterprise) installation:
Finished-product pass rate: 87% → 99.2%
Resin-content deviation: controlled within ±1.5%
Single-batch capacity: increased by 40%, delivery cycle shortened by 25%
Overall production cost: reduced by 12.6% (energy saving + loss reduction + low maintenance)
End-component mechanical properties: tensile/peel strength increased by over 12%, passing review by a leading new-energy enterprise
Customisation Service Notes
KLT supports 100 T–500 T tonnage customisation, work-table size customisation, multi-layer hot-press structure customisation and explosion-proof / high-temperature-reinforced version customisation; it can be combined with automatic loading, automatic demoulding and production-line linkage modules to build a fully automated prepreg hot-press forming line. With original-factory non-standard process adaptation, lifetime technical consultation and regular equipment inspection, it helps composite enterprises achieve high-quality, low-cost mass production.
Equipment images and parameters are supplied product references. Final configuration and process performance are confirmed in the technical proposal.
← All carbon-fiber equipment